AI Vision Systems: Discover Core Technologies Behind Visual Inspection
Manufacturing quality often depends on finding small defects before products leave the production line.
AI vision systems combine industrial cameras, lighting, image processing, and machine learning to examine products automatically and identify visual characteristics that may be difficult to evaluate consistently by manual inspection.
These systems are becoming increasingly useful across electronics, automotive components, packaging, food production, pharmaceuticals, and other manufacturing environments. Improvements in imaging hardware and artificial intelligence allow inspection systems to handle more complex visual variation while maintaining high-speed production workflows.
Understanding the technology behind AI-powered visual inspection helps explain why these systems can recognize defects, classify products, verify assembly, and support process control. The key is not AI alone, but the way several technologies work together from image capture through decision-making.
How AI Vision Systems Fit Into Visual Inspection
A conventional machine vision system typically captures an image, processes it using predefined rules, and determines whether an object meets specified criteria. AI vision adds machine learning models that can identify patterns from examples rather than depending entirely on manually defined inspection rules.
The system still begins with image acquisition. A camera captures the object under controlled lighting, and software converts the image into information that can be analyzed.
The AI model then evaluates relevant visual characteristics. Depending on the application, it may detect surface defects, classify objects, locate components, identify missing parts, or determine whether an assembly matches the expected configuration.
The final result can be passed to a production-control system. A defective product may be rejected, an operator may receive an alert, or inspection results may be stored for quality analysis.
Cameras and Imaging Hardware Provide the Foundation
AI cannot make a reliable decision if the captured image does not contain enough useful information. Camera selection is therefore one of the most important parts of a visual inspection system.
Industrial cameras may use different sensor types, resolutions, frame rates, and optical configurations depending on the inspection task. A system inspecting a rapidly moving production line may require high-speed image capture, while a precision electronics application may prioritize fine spatial detail.
Lens selection also matters. The lens determines factors such as field of view, magnification, working distance, and image distortion. A poorly matched lens can make an otherwise capable AI model difficult to use effectively.
In some applications, specialized imaging technologies are useful. Monochrome cameras can provide strong contrast for certain inspection tasks, while color cameras can distinguish visual differences that grayscale imaging cannot capture.
Lighting Determines What the Camera Can See
Lighting is often underestimated when designing AI vision systems. Even sophisticated AI models depend on images with sufficient contrast and consistent visual characteristics.
The objective is not simply to make the product brighter. Lighting should emphasize the features that the inspection system needs to recognize while reducing unwanted reflections, shadows, and background variation.
Different arrangements can serve different inspection requirements. Backlighting can highlight silhouettes and dimensional outlines, while directional lighting can make surface features more visible. Diffuse lighting can help reduce harsh reflections on certain materials.
Consistent illumination is particularly important for machine learning. If lighting changes significantly between training images and production images, the model may interpret environmental variation as a product characteristic.
Image Processing Turns Visual Data Into Useful Information
Before an AI model analyzes an image, the system may perform several processing operations. These can include cropping, resizing, contrast adjustment, noise reduction, geometric correction, or region-of-interest selection.
The purpose is to provide the model with relevant information while reducing unnecessary visual variation.
Traditional image-processing techniques can still be valuable alongside AI. For example, simple thresholding or edge detection may reliably identify a defined geometric feature, while a machine learning model handles more variable surface defects.
This combination can be more practical than relying exclusively on artificial intelligence. A well-designed inspection system uses the simplest reliable technique for each part of the task.
Machine Learning Enables More Flexible Inspection
The main distinction between conventional machine vision and AI vision is how visual decisions are developed.
Traditional systems often depend on explicitly programmed rules. Engineers define thresholds, measurements, shapes, or patterns that determine whether an item passes inspection.
Machine learning systems can instead learn patterns from representative training data. A model may be trained using images of acceptable products and examples containing relevant defects or variations.
This approach can be useful when defects are difficult to describe through fixed rules. Scratches, irregular textures, subtle assembly differences, and inconsistent surface patterns may not have a single straightforward visual threshold.
However, AI does not remove the need for engineering judgment. Training data must represent the actual production environment, and the model needs to be evaluated against realistic inspection conditions.
Key AI Technologies Used in Visual Inspection
Different AI techniques address different visual tasks.
Image classification determines which category an image belongs to. For example, a system could classify components as acceptable or defective.
Object detection identifies specific objects within an image and determines their locations. This can be useful when several components appear within the same inspection frame.
Image segmentation goes further by identifying individual pixels associated with an object or defect. This can help measure the exact area or shape of a surface irregularity.
Anomaly detection is useful when defective examples are limited. Instead of learning every possible defect, the system can learn the normal appearance of products and identify significant deviations.
The appropriate technique depends on the inspection objective, available data, product variation, and required decision precision.
Training Data Is Central to AI Inspection
A machine learning model is only as useful as the information used to develop and evaluate it. Industrial inspection therefore requires careful attention to image datasets.
Images should represent normal production conditions rather than idealized laboratory environments. Variations in lighting, product orientation, surface appearance, acceptable tolerances, and equipment conditions can all influence model performance.
Defect examples also need appropriate representation. If a particular defect occurs rarely, collecting enough meaningful examples can be difficult. Synthetic or augmented data may sometimes supplement real images, but it should not replace appropriate validation using actual production conditions.
Data labeling is another important step. Images may need to be annotated with defect locations, object boundaries, categories, or other information required by the selected model.
From Detection to Production-Line Decisions
AI inspection becomes operationally valuable when its visual decisions connect reliably with manufacturing equipment.
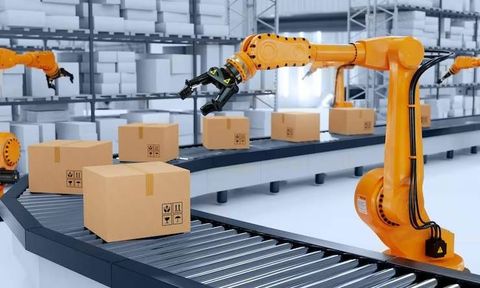
A typical workflow may involve a sensor detecting that an item has entered the inspection area. The camera captures one or more images, the vision system processes them, and the AI model evaluates the relevant characteristics.
The resulting decision can then be communicated to a programmable logic controller or another production-control system. If the item fails inspection, a mechanical rejection mechanism can remove it from the production flow.
Inspection results can also be recorded for quality monitoring. Over time, this information may reveal recurring defect patterns or changes in process performance.
Where AI Vision Provides the Most Value
AI-powered inspection is particularly useful where products contain visual variation that is difficult to evaluate consistently through fixed rules or manual inspection.
Common applications include:
- Surface defect detection
- Assembly verification
- Component presence and placement
- Label and print inspection
- Packaging inspection
- Product classification
- Dimensional or positional verification
- Detection of unusual visual patterns
The technology can also support traceability by associating inspection results with production batches, timestamps, equipment conditions, or individual products when appropriate.
Challenges That Affect System Performance
AI vision systems are not automatically accurate simply because they use advanced models. Real-world performance depends on the entire inspection environment.
Poor lighting, camera vibration, lens contamination, changing product orientation, reflective surfaces, and unexpected product variation can reduce reliability. A model trained on limited data may also struggle when exposed to conditions it has not encountered before.
False positives and false negatives require particular attention. Rejecting acceptable products unnecessarily can disrupt production, while failing to identify genuine defects can undermine quality control.
For this reason, successful deployment usually involves ongoing validation, model monitoring, controlled imaging conditions, and periodic review of inspection results.
FAQ: AI Vision Systems and Visual Inspection
What is an AI vision system?
An AI vision system uses cameras, lighting, image-processing technology, and artificial intelligence to analyze visual information and make inspection or classification decisions.
How is AI vision different from traditional machine vision?
Traditional machine vision often relies heavily on predefined rules and thresholds. AI vision can learn visual patterns from training data, making it useful for more variable or difficult-to-define inspection tasks.
Can AI vision detect manufacturing defects?
Yes. Depending on the system and training data, AI vision can identify defects such as scratches, surface irregularities, missing components, incorrect assembly, contamination, and other visual abnormalities.
Does an AI vision system need controlled lighting?
Yes. Consistent lighting is extremely important because changes in illumination can alter the appearance of products and affect model performance.
Can AI vision replace human quality inspectors?
Not necessarily. AI vision can automate repetitive inspection tasks and support human quality teams, but many manufacturing environments still require human oversight, especially for complex decisions and process management.
Conclusion
AI vision systems bring together imaging hardware, controlled lighting, image processing, machine learning, and production controls to create automated visual inspection workflows. Their effectiveness depends on how well these components are designed as a complete system.
The most capable solution is not simply the one with the most advanced AI model. Reliable inspection comes from appropriate cameras and optics, consistent illumination, representative training data, suitable algorithms, robust validation, and dependable integration with production equipment. When these elements work together, AI vision can make visual quality inspection more consistent, measurable, and adaptable to modern manufacturing requirements.
Related Post...
Dedicated Enterprise Secure Fiber Leased Lines: Explore Modern Network Architecture
Updated: October 06, 2026
Read More
Corporate Multi-Agent AI Orchestration Systems: Discover How Agents Work Together
Updated: October 06, 2026
Read More
AI Vision Systems: Discover Core Technologies Behind Visual Inspection
Updated: October 06, 2026
Read More